Hey there, if you’re hunting for graphite rods—whether for aerospace parts, lab furnaces, EDM tools, or even that custom DIY project you’ve been tinkering with—you already know this stuff is versatile as hell. But here’s the thing most people skip over at first: the surface finish of your graphite rod isn’t just a cosmetic detail. It’s the difference between a part that holds up under high heat, doesn’t leave unwanted residue, or actually fits the job at hand, and one that gets tossed in the scrap bin faster than you can reload a prototype. As a graphite rod supplier who’s been deep in this game for years, I’ve talked to dozens of clients who ordered the exact size they needed but blew it on the finish, so let’s break down all the real, usable surface options out there—no stuffy textbook jargon, just what actually works. Graphite Rod

First, let’s start with the “base” finish, because everyone orders this default one sometimes. Raw graphite as it comes right out of the mold or extruder is called as-machined (or “as-sintered,” if we’re being specific but keeping it casual) finish. Wait, let’s call it raw machined finish, that’s easier. This is the one with tiny, almost microscopic ridges from the cutting tools—like super fine sandpaper grit, way smoother than wood but not by much. It’s porous, too, a little bit. Why would anyone pick this? It’s cheap, obviously. For basic, low-stress jobs where you’re just holding the rod (like a simple support stand for a small beaker in a high school lab), it’s perfect. The porous part doesn’t matter here because there’s no chemical or high-heat load pushing on it. But here’s the catch: if you’re using this in a furnace, those tiny pores can trap air or impurities that might outgas when you crank up the heat, which could mess with your process. And if you’re using it for EDM (electrical discharge machining) electrodes? That rough surface might leave tiny, uneven marks on the metal part you’re cutting, which is a big no-no for precision parts. I’ve had a few CNC shops come back to me saying they ordered raw rods and the finish was too rough for their work—always good to flag that upfront.
Next up, if you want to smooth those raw edges without spending a ton, we have ground finish. This is when we run the raw rod through a grinding wheel, kind of like how you’d sand down a piece of wood to get rid of splinters. The key here is the grit size of the grinding wheel—we can do anything from 60 grit (which leaves a slight, uniform texture) up to 1000 grit (super smooth, almost like glass to the touch). Why would someone go for this over raw? It’s still cheaper than the fancier finishes, but it fixes the porosity a little bit—wait, no, actually, grinding can even out the surface pores so they’re less deep, which reduces outgassing. For low to mid-temperature furnaces (think up to 1500°C, roughly 2700°F), this is a solid pick. It’s also great for general EDM electrodes that don’t need the absolute mirror finish—like for larger parts where tiny surface inconsistencies won’t show up. I recommend ground finish more than raw for most first-time buyers, unless they’re on a super tight budget for a one-off test.
Now, let’s get into the ones that are for when you need to step up the performance: polished finish. This is where we take the ground rod and buff it with finer and finer abrasives until it’s literally smooth enough to see your reflection. Wait, not a literal mirror, but way smoother than ground. The grit here is usually 1200 to 2000 grit, so those tiny ridges from grinding are gone entirely. Polished finish is non-porous for all practical purposes, so it barely outgasses at all—perfect for high-temperature furnaces (like 2000°C or higher), vacuum applications, or processes where even the tiniest amount of residue is a problem. Think semiconductor manufacturing, or metal heat treating where purity is everything. I had a client a while back making components for a solar panel fab line that ordered polished rods, and he told me it cut his cleaning time in half because there was no gunk stuck to the surface. The only downside? Polished rods cost a bit more, and they’re a little more fragile—because the super smooth surface is more prone to scratching if you mishandle them. So you don’t want to drag these across a workbench, keep them wrapped in the plastic we send them in until you’re ready to use.
Wait, there’s another finish that’s really useful for high-temperature or chemically harsh environments: coated graphite rods. Wait, hold on—coating is technically a surface finish treatment, right? Because you’re adding a layer on top of the graphite. The most common coating we do is silicon carbide (SiC) coating, sometimes called CVD (chemical vapor deposition) coating, though we just call it SiC coating for short. What does that do? It’s a thin, hard, super inert layer that seals the graphite surface completely. No more porosity, no more outgassing, and it protects the graphite from reacting with chemicals—acids, alkalis, even some molten metals. For example, if you’re using a graphite rod in a crucible to melt aluminum, uncoated graphite would react with the aluminum and cause impurities in the final metal. A SiC coated rod? That eliminates that problem. We also do other coatings, like pyrolytic graphite (PG) coating, which is even harder and has higher thermal conductivity—great for heat exchangers or high-power EDM. The thing about coated finishes is they’re not just smooth, they’re functional. They let you use graphite in jobs you couldn’t even touch with uncoated material. The downside is, yeah, they’re more expensive, and you have to make sure the coating is applied evenly—we check every coated rod under a microscope to make sure there are no thin spots, because a tiny crack in the coating is a weak point.
Wait, did I miss a common one? Oh right, dimensional finish—wait no, sometimes people mention precision machined finish, which is when we not only smooth the surface but get the diameter super exact, like within a few thousandths of an inch. That’s huge for things like sliding bearings or guides, where a rod that’s even a tiny bit off diameter won’t fit right. I’ve had a few machine shops order “precision finished” rods because their old ones were so out of spec they kept jamming their machines. That’s different from polished, because it’s less about surface smoothness and more about tight tolerances on shape.
Let me also talk about when to avoid which finishes, because that’s the part most supplier blogs skip. For example, if you’re using graphite for a hobby project—say, a DIY battery electrode—polished or coated is total overkill. You’d be wasting money. Raw or ground is more than enough, and it’s cheaper. On the flip side, if you’re working in a vacuum furnace, don’t order raw—those pores will off-gas water and other gasses that can mess with the vacuum, making your process longer and less efficient. And for metal melting, always go coated, unless you want extra impurities in your material.
As a supplier, the first question I ask every client is: “What are you using this rod for, and what environment is it going in?” Because that’s how we pick the right finish. I’ve had a client come to me once asking for rods for a furnace at 1800°C—they ordered raw because it was cheaper, and by the time they got to the job, they were seeing way more outgassing than expected. We exchanged them for ground rods, which helped a little, but once they moved to polished, they were good. Another guy needed rods for an EDM electrode for a medical part, so polished was non-negotiable—any scratch would get rejected by the client’s quality team.
Wait, also, let’s address a common myth I hear all the time: “All graphite rods are the same, so finish doesn’t matter.” Dude, I’ve seen this firsthand. Last year, a aerospace parts maker ordered a batch of uncoated graphite rods to use in a jet engine test rig. The uncoated ones reacted with the hot exhaust gases, leaving a residue that clogged a valve. We sent them coated rods, and that same valve stayed clear for months. That’s not a trivial difference—that’s part performance, part safety.
Let me wrap this up with a quick cheat sheet, so you can reference it if you’re ever ordering:
- Raw Finish: Budget, low-stress jobs, not for high heat/purity.
- Ground Finish: Mid-budget, smooths raw, reduces porosity, good for furnaces, general EDM.
- Polished Finish: High-purity, high heat, vacuum, precision EDM, minimal residue.
- Coated Finish (SiC, PG): Harsh chemicals, molten metals, extreme heat, maximum protection.
- Precision Finish: Tight tolerances, sliding/guiding applications.
If you’re still not sure which one is right for your project, don’t guess. Reach out to me—we’ll talk through what you’re making, the temperature, chemicals, tolerances, all the details, and I’ll point you to the finish that works best. No pressure, no hard sell, just straight talk from a guy who’s been selling graphite rods long enough to know when a client is overspending or underspending on a finish they don’t need. I’m here to help you get the right part for your job, not just another sale.
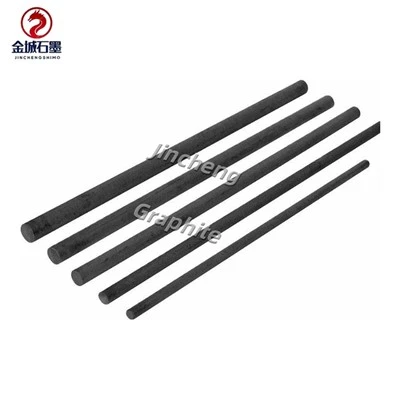
Now, if you’re ready to lock in a batch, or even just have questions about specific applications, get in touch. We can talk specs, quantities, delivery timelines, whatever you need. No weird fine print, no hidden fees, just quality graphite rods with the right finish for your use case.
Wafer Graphite Carrier References:
- “Graphite Surface Finishes and Their Applications”, Carbon Products Division, National Institute of Standards and Technology (NIST)
- “Pyrolytic and Silicon Carbide Coatings for Graphite Components”, Journal of Carbon Materials Science, 2022
- “Surface Roughness Effects on Graphite Electrode Performance in EDM”, International Journal of Machine Tools and Manufacture, 2019
- “Outgassing Properties of Graphite Rods for High-Temperature Vacuum Processes”, Vacuum Technology & Coating Magazine, 2021
Huixian Jincheng Abrasive Mold Factory
As one of the most professional graphite rod manufacturers and suppliers in China, we have world-leading production equipment and strong manufacturing capabilities. Please rest assured to buy durable graphite rod for sale here from our factory. Quality products and reasonable price are available.
Address: Mengzhuang Town, Huixian City, Henan Province
E-mail: graphite.jc@gmail.com
WebSite: https://www.graphite-jc.com/
