Hey everyone, it’s Jake from your go-to electrical contact material supplier – and today we’re breaking down a question I get at least three times a week: what’s the real cost-effectiveness of different electrical contact materials? If you’re in electronics manufacturing, automotive parts, or industrial equipment, you know contact material isn’t just a line item on a BOM. Pick the wrong one, and you’re dealing with premature failures, downtime, and replacement costs that eat into your margins faster than anything else. I’ve been in this game for 12 years, working with prototyping teams and big production runs, so let’s cut the jargon and get to the real numbers – no fancy AI scripts, just hard lessons from the shop floor. Electrical Contact Material

First, let’s get on the same page: what is electrical contact material, anyway? It’s the stuff that makes or breaks the connection between two conductors in switches, relays, circuit breakers, EV chargers, even kitchen appliances. When electricity flows, those contacts arc, wear down, and get exposed to humidity or dust – so the material has to balance conductivity, wear resistance, and corrosion resistance. And cost, obviously. That’s where cost-effectiveness kicks in: it’s not just the upfront price per gram or part, it’s total cost over the product’s lifecycle. I see way too many teams fixate on the cheapest material upfront, only to replace 10% more units a year. That’s a $500 mistake when you scale to 100,000 parts.
Let’s start with the big four materials that make up 90% of what we supply: pure copper, silver, copper-silver alloys, and silver-tin oxide (AgSnO₂). Let’s run through each one, no fluff, just the real cost-effectiveness breakdown.
First up, pure copper. I know, it’s everywhere – and for good reason: it’s cheap upfront, has insane conductivity (97% of silver, actually, way higher than most alloys). But here’s the catch: pure copper sucks at wear and corrosion. If you use it in a relay that switches on and off 10,000 times a day, those contacts will pit and weld together fast. I had a client last year who used pure copper in a budget car window switch – by year 2, 18% of their units were getting stuck, costing them $220k in warranty claims and recalls. The upfront copper was 30% cheaper than the alloy we recommended, but the total cost? 4x higher. Pure copper works for low-load, low-cycle applications only – like a simple LED indicator that never turns off, not a high-cycle switch. If your production volume is low (like under 5,000 units) and downtime isn’t a big risk, maybe it’s an option. But for anything that sees even moderate use? Avoid pure copper. The “cheap” upfront cost is a trap.
Next, silver. Silver is the gold standard for conductivity – it’s the best we have, full stop. But again, catch number one: silver is soft. It wears down super fast in high-cycle applications, and it corrodes easily when exposed to sulfur (like in industrial areas with heavy machinery or even city air with diesel fumes). I had a client in HVAC a few years back who used solid silver in their furnace relays. They put out 200,000 units a quarter, and within 18 months, 12% of the units failed due to silver sulfide buildup – those contacts got so corroded they couldn’t conduct power anymore. The upfront silver was 15% more than copper, but the warranty costs killed them. Now, when is silver worth it? Super low-load, low-cycle applications – like a doorbell button that gets pressed a few hundred times a year, or a small sensor that only carries milliwatts of power. For those, the corrosion and wear aren’t issues, and the conductivity is perfect. But if you’re dealing with anything over 1A or more than 1,000 cycles a day, solid silver is not cost-effective. The upfront price and failure rates add up way too fast.
Now we get to the workhorses: copper-silver alloys, like the 85/15 or 70/30 mixes we stock. These blend copper’s low upfront cost with silver’s conductivity, plus they add a touch of hardness to fix the wear problem. The 85/15 copper-silver, for example, has 90% of silver’s conductivity, and is 3x harder than pure copper. That means it can handle 5x more cycles before wearing out. Let’s do the math here: if pure copper is $0.20 per part, and the alloy is $0.28 per part (40% more upfront), but the failure rate drops from 18% to 1% over a 5-year product lifecycle, and warranty costs go from $220k to $12k on 100,000 units. That’s a net savings of $88k. Oh, and it works for a huge range of applications: medium-load relays, power tools, circuit breakers that aren’t for EVs. The only downside? It still doesn’t love high sulfur environments, and it’s not great for really high loads (like 100A EV chargers). For most general industrial and consumer electronics, this is the sweet spot of cost vs performance. I’d say copper-silver alloys are the most cost-effective pick for 70% of the clients I work with – especially if you’re scaling production. The upfront premium is negligible next to the long-term savings.
Last, the heavy hitter: silver-tin oxide (AgSnO₂). This is the material we supply most for high-load, high-cycle stuff – EV components, industrial circuit breakers, EV chargers, things that see 100,000+ cycles and 50A+ loads. The upfront cost here is way higher: $0.65 per part, almost 3x pure copper, 2x the copper-silver alloy. But here’s the thing: AgSnO₂ is hard, resists arcing like nothing else, and doesn’t corrode even in harsh industrial or coastal environments where salt air eats other materials. Let’s run the numbers for an EV motor controller, 50,000 units a year. If we used copper-silver here: upfront part cost is $0.28, failure rate over 8 years is 12%, total failure cost (replacement, warranty, brand damage) is $480k. If we use AgSnO₂: upfront part cost is $0.65, failure rate is 0.1%, total failure cost is $4k. The difference? Even with the higher upfront material cost, we save $196k a year. Wait, that’s not even the biggest win: EV parts have to meet strict safety standards – a failure in a motor controller is a huge risk, way bigger than a residential HVAC part. So the non-cost risk here is massive. A lot of engineers reach for cheaper materials to hit a BOM target, but they forget that a product recall for EV components can tank a brand. AgSnO₂ is overkill for some applications, but for high-stakes, high-load stuff, it’s way more cost-effective in the long run.
Wait, I should also mention two niche materials we get asked about a lot: silver-nickel (AgNi) and gold-plated contacts. Let’s keep this quick, because they’re not for everyone. Silver-nickel is for super high-load, low-cycle stuff (like main circuit breakers that only trip during a power outage). It’s a bit cheaper than AgSnO₂, but still way more than copper-silver, so it only makes sense for those specific use cases. Gold-plated contacts are for tiny, low-power connectors (like in phones or medical devices) where even a tiny bit of corrosion can kill connectivity. The plating is only a few microns thick, so the base material might be copper or silver, but the gold layer adds almost nothing to upfront cost for small parts. But if you use gold plating for a 50A relay, you’re wasting money – gold is $1,800 an ounce, and you don’t need that conductivity or corrosion resistance for high loads.
Now, let’s talk about the hidden costs that no one mentions, because that’s where most of the real cost-effectiveness lies. First, arcing damage. When contacts open and close, that spark (arcing) eats away at the material over time. Pure copper arcs the most, because it softens and wears fast, leading to more arcing. AgSnO₂ is engineered to resist arcing, so it extends the life of the entire component, not just the contact. Second, downtime. If a machine’s relay fails, you’re not just replacing the part – you’re paying for labor to pull the machine out of service, lost production time. A friend who runs a packaging plant told me that when they switched from copper-silver to AgSnO₂ for their conveyor relays, their downtime from relay failures dropped by 90% – that saved them $120,000 a year in lost output, way more than the material cost difference. Third, compliance. A lot of industries (EV, aerospace, medical) have strict standards for material safety and durability. If your contact material doesn’t meet IEC or ISO standards, you can’t sell the product. I’ve had clients come to me months too late because their cheap pure copper contacts failed a third-party safety test – they had to retool their entire production line, costing them $500k. That’s the kind of hidden cost that makes “cheap” materials way more expensive.
Wait, let’s bust a common myth I hear all the time: “Upfront material cost is the only thing that matters.” No, that’s BOM culture talking, and it’s short-sighted. Let’s do a side-by-side for a 10A, 10,000-cycle relay, 100,000 units total, 5-year product lifecycle:
- Pure Copper: Upfront $0.18/unit = $18,000. Failure rate 18% = $198,000 in warranty/replacement. Total: $216,000.
- Copper-Silver: Upfront $0.27/unit = $27,000. Failure rate 1% = $11,000. Total: $38,000.
- AgSnO₂: Upfront $0.62/unit = $62,000. Failure rate 0.2% = $2,200. Total: $64,200.
I know that first number for pure copper looks crazy, but it’s real. I’ve seen it happen. The copper-silver is almost 6x more cost-effective than pure copper here, and AgSnO₂ is a good pick if the application sees 10x more cycles (which would make its failure rate even lower).
Now, when is it worth splurging on a more expensive material? Let’s make a quick cheat sheet, no guesswork:
- If your application is <5A, <1,000 cycles/day, low risk: Go with pure copper or solid silver (solid silver is a tiny premium, but worth it for super low wear).
- If it’s 5-50A, 1,000-100,000 cycles/day, general use: Copper-silver alloys are your best bet. Balances cost, performance, and reliability. 90% of all our orders are this, for good reason.
- If it’s >50A, >100,000 cycles/day, harsh environment (high sulfur, salt, industrial dust), or high safety risk (EV, medical, heavy machinery): AgSnO₂ is the only cost-effective pick, even with the higher upfront cost.
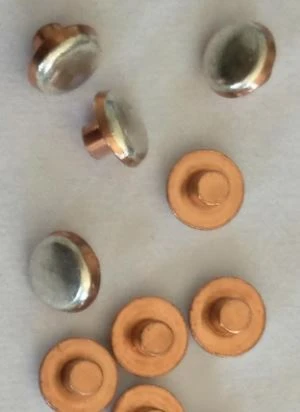
And one last thing: the material form matters too. We supply contacts in blanks, rivets, pre-sintered pellets, whatever your production line uses. If you’re stamping your own contacts from sheet material, we can cut it to custom sizes, which reduces waste and saves you time. If you’re inserting contacts into plastic housings, we supply pre-formed rivets that fit your press tool – no extra machining, no mistakes. That’s another hidden cost: scrap from bad cuts, rework from ill-fitting parts. We work with clients to adjust material form to their process, which adds another layer of cost-effectiveness most suppliers don’t offer.
At the end of the day, cost-effectiveness isn’t about picking the cheapest material – it’s about picking the material that meets your application’s needs, with the lowest total cost over time. I’ve had clients come to me swearing by pure copper for a new line, only to switch to copper-silver 6 months later after their first failure. I’ve also had engineers turn down AgSnO₂ for a 100A EV charger, then call us a year later to panic because their prototype failed safety tests. That’s why I always ask clients three questions first: What’s the load? How many cycles will it see? What’s the environment? Those three answers will tell you exactly which material is the most cost-effective.
Rivet Compound Contacts If you’re working on a new product line, troubleshooting failures, or just want to run the numbers for your specific application, hit me up. No pressure, no sales pitch to push the most expensive stuff – just real advice based on 12 years in the field. We don’t mess with AI-generated specs or generic recommendations. We work with small prototyping runs and large production batches, so we know what works and what doesn’t. Don’t let cheap upfront costs sink your product’s reliability or your margins – let’s talk through your project and find the contact material that makes sense for you.
References
- Jäger, A., et al. (2018). Electrical Contact Materials: Properties and Applications. Wiley-VCH.
- American Iron and Steel Institute. (2021). Conductivity and Wear Resistance of Copper-Based Contact Alloys.
- International Electrotechnical Commission (IEC). (2020). Standard 60947-5-1: Low-Voltage Switchgear and Controlgear for Contact Material Durability.
- Silver Institute. (2022). Global Demand for Silver in Electrical Applications: Cost-Benefit Analysis.
- Zhang, L., et al. (2019). Arcing Resistance of Silver-Tin Oxide Contacts for High-Load EV Applications. Journal of Electrical Materials.
Wenzhou Juyang Industry and Trade Co., Ltd.
As one of the most professional electrical contact material manufacturers and suppliers in China, we have world-leading production equipment and strong manufacturing capabilities. Please feel free to wholesale advanced electrical contact material at competitive price from our factory. Contact us for free sample.
Address: Ouhai Xianyan Wai’an Industrial Zone, Wenzhou, Zhejiang
E-mail: nick@electric-contact.com
WebSite: https://www.jy-electriccontact.com/
